
Crankshaft high-speed external milling is a CNC roughing process in which a large disc milling cutter, turning on an axis parallel to the crankshaft, cuts the main journals, crankpins and web faces while the crankshaft itself rotates slowly. The cutting speed comes from the cutter, not from the workpiece. Because the crankshaft is driven as a controlled rotary axis, the cutter can follow each off-center crankpin with its X axis, so pins at different angles are machined without re-chucking the part on each pin axis.
This guide is written for process engineers, production managers and equipment buyers who are planning or upgrading a crankshaft line. It explains how the cutter follows a crankpin, where milling sits in the crankshaft machining process, how it differs from turning, turn-broaching and internal milling, which cutting parameters matter, and what to check on a machine specification. The numbers in this article come from two published patents on crankshaft milling, a university thesis on crankshaft production, UBright's own machine catalog, or calculations shown in the text. Patent figures are the applicants' preferred ranges, not independent test results, and they are presented that way.
Key takeaways
- In external milling the cutter supplies the cutting speed while the crankshaft turns slowly, so the crankshaft rotation can be used as a controlled C axis.
- Following a crankpin needs synchronized C-axis rotation and X-axis cutter motion; turning and turn-broaching run the part too fast for that.
- Patent guidance puts chip thickness first and then keeps cutting speed as high as tool life allows.
- Milling is a roughing step. In the conventional route the journals are hardened and then ground to size.
- Read a machine's cutter diameter, spindle speeds and C-axis repeatability together; they set the cutting speed and the pin contour.
Table of Contents
- What is crankshaft high-speed external milling?
- How the X–C linkage tracks each crankpin
- Where milling sits in the crankshaft machining process
- External milling vs turning, turn-broaching and internal milling
- Crankpin milling parameters: cutting speed and chip thickness
- The disc milling cutter and its inserts
- Accuracy and contour control
- Choosing crankshaft high-speed external milling equipment
- Frequently asked questions
- Summary
- Discuss your crankshaft machining project
What is crankshaft high-speed external milling?
External milling uses a disc-shaped tool with cutting edges around its whole periphery. US patent 6,684,500 describes the tool as drivable in rotation on an axis parallel to the workpiece axis. In this process the cutting speed results primarily from the rotation of the tool, while the workpiece turns at only about 10 rpm until the tool has made at least one complete pass around the surface being machined. When the stock to be removed is large, several passes may be needed. Even a single pass often takes more than one full revolution, because the cutter has to move in and out tangentially.
The same patent sets out why this matters for crankshafts. In turning and turn-broaching the part spins fast, so its angle does not need to be monitored and the tool cannot track it in X. In external milling the crankshaft turns slowly, and a controlled C axis becomes an absolute necessity because the crankpins have to be machined. That C axis is what lets the cutter follow a pin that is orbiting the main-journal axis.
Main journals, crankpins and webs
A crankshaft carries several kinds of surfaces that a milling process has to reach. The main journals lie on the axis the crankshaft rotates about. The crankpins, also called big-end or connecting-rod journals, are offset from that axis by the crank throw. The webs connect them, and their side faces and outer contour are also machined. US patent 6,283,687 lists separate insert designs for journal surfaces, web faces and the undercuts at the transition between a journal and a web, which shows how many surface types one cutter body may have to cover.
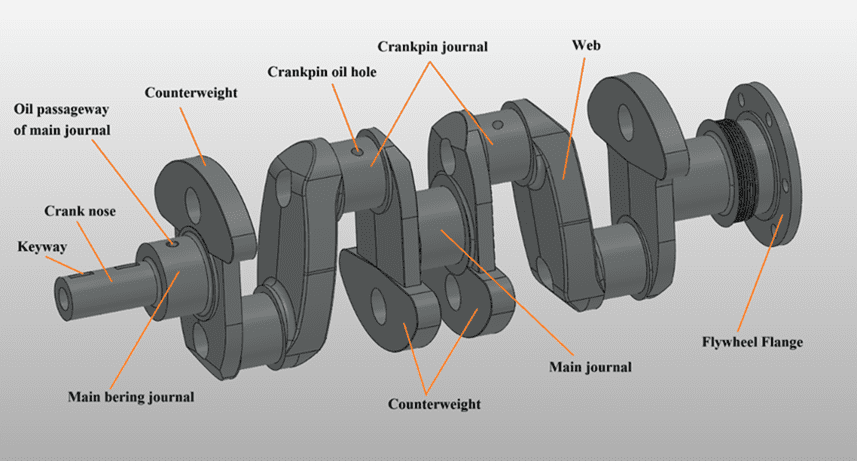
The crankshaft is also a weak workpiece. US 6,283,687 points out that the eccentric surfaces and the shape of the part make straight crankshafts demanding to machine. Most of the process choices below follow from that: keeping cutting forces low, supporting the part well, and controlling how the cutter enters and leaves each journal.
What makes crankshaft external milling high-speed
"High-speed" refers to cutting speed. US 6,684,500 gives example thresholds for high-speed milling: over 130 m/min for steel, in particular over 180 m/min; over 150 m/min for cast iron, in particular over 200 m/min; and over 300 m/min for aluminum, in particular over 500 m/min. According to the patent, these speeds are made possible mainly by a positive cutting-edge geometry and a suitable choice of cutting material. It adds that the high cutting speed reduces the drawbacks of the interrupted cut that is inherent in milling.
US 6,283,687 describes the same development: with positive tool geometry and specific insert materials and coatings, high-speed milling can reach 350–500 m/min and sometimes more. The words "high-speed" therefore say nothing about workpiece rotation, which stays slow. They describe the peripheral speed of the cutter.
How the X–C linkage tracks each crankpin
The crankshaft is chucked on its main-journal axis and turned by the machine as the C axis. When the cutter works on a main journal, the journal is concentric with the C axis and the cutter only has to feed to depth. When it works on a crankpin, the pin orbits the main-journal axis. The cutter must then move along X in step with the crank angle so that it stays in contact with the pin surface. The pin contour is generated by this coordinated C and X motion.
US 6,283,687 notes why external milling suits this better than processes that rely on fast workpiece rotation. When the cutting speed comes from a rapidly turning crankshaft, a tool unit following a pin would have to move just as rapidly in X, and possibly in Y. With slow workpiece rotation, the X motion becomes manageable, and separate cutters can work on pins at different angles. The patent also prefers external milling because the tool is easier to handle and because it can produce planar outer surfaces on the part.
Climb milling and the shape of the chip
The patent recommends milling by the climb-cutting method wherever possible. The cutter and the workpiece surface move in the same direction at the machining point. In the patent's figure the cutter turns anticlockwise and the crankshaft clockwise.
Each cutting edge removes a chip shaped like a flat, irregular triangle. Its thickness rises quickly to a maximum and then falls slowly toward the end of the cut. At constant stock and constant workpiece speed, lowering the cutter speed lengthens the distance between successive edge strikes on the workpiece, which increases the maximum chip thickness. The patent explains its preference for climb cutting this way: with a thin average chip and a positive tool geometry, the cutting forces put only relatively low dynamic loads into the part, despite the interrupted cut, and lateral deflection of the workpiece is largely avoided.
Entering and leaving the cut
Plunging straight to size would be harmful. A disc cutter turning on an axis parallel to the journal wraps a long arc of contact, so a fast radial infeed would raise the chip thickness and the transverse force on the part. US 6,283,687 therefore feeds the cutter slowly to the final radial dimension while the crankshaft keeps turning. The stock is fully engaged only after the journal has turned through about 50–70°, preferably about 60°.
From that point the cutter makes a complete revolution of the journal and slightly more, about 370°, to bring the actual contour onto the target contour. It then retracts directly outward. In the patent's broader statement of the method, the journal turns through 30–90°, preferably 50–70°, during the slow infeed. The point is to respect the chip-thickness limit from the first contact, so that no excessive transverse force reaches the workpiece.
Where milling sits in the crankshaft machining process
US 6,283,687 describes the usual crankshaft machining process in three steps. Crankshafts are rough-machined with defined cutting edges, by turning, milling, turn-broaching and similar processes. The journal surfaces are then hardened. Finally the journals are precision-machined to size by grinding. Macerol's 2019 thesis on crankshaft grinding describes the same order for high-end crankshafts, including those for heavy-duty vehicles: forged, machined, heat treated and then ground. Grinding is one of the last operations, so it carries much of the responsibility for the final geometry and surface integrity.
External milling therefore prepares the part for grinding rather than replacing it. The stock it leaves, the roundness of the pins and the condition of the undercuts all affect the following grinding step. That step is covered in our guide to crankshaft following grinding, where the grinding wheel follows each pin with the same kind of C and X linkage used in milling.
The same machining principle is used on camshafts, which US 6,684,500 names alongside crankshafts as typical workpieces. Our article on the camshaft machining process covers the milling and CBN grinding of cam profiles.
Milling before or after hardening
US 6,283,687 also describes high-speed milling of crankshafts that are already hardened, for example to 60–62 HRC. The patent's argument is that machining after hardening removes the distortion caused by hardening during the cutting step itself. Where high-speed milling of the hardened part gives a surface acceptable as the final state, it says at least the rough-grinding operation can be dropped.
That claim stops short of finish grinding. A buyer evaluating hard milling should ask which journals and surfaces the supplier expects to leave unground, and what tolerance and surface data support that for the specific part.
External milling vs turning, turn-broaching and internal milling
Several defined-edge processes compete for the same crankshaft surfaces. US 6,684,500 sets out the terms, and US 6,283,687 explains why mass production has used different processes for different surfaces. In the arrangement both patents describe, main bearings are machined by rotational broaching or turn-broaching. Crankpins, and sometimes the web side faces, are machined by external milling, internal milling or a related milling method.
Turning and turn-broaching on the main journals
In rotational broaching, the cutting edges sit around a disc-shaped tool whose axis is parallel to the crankshaft. The edges are spaced at increasing distances from the tool center. The crankshaft turns much faster than the tool, and US 6,684,500 gives about 1000 rpm for a passenger-car crankshaft against less than 30 rpm for the tool. Turn-broaching adds a plunge-cut turning step before the broaching. In that step an edge on the same disc is fed radially into the part while the disc does not rotate.
US 6,283,687 describes rotary turn-broaching as established for the main bearings, with the crankshaft chucked on its main-journal axis and turned rapidly. The end faces of the webs are generally machined at the same time. To turn-broach the crankpins, the part would have to be chucked eccentrically on each pin axis, which is far more complicated than chucking it on the main-journal axis.
Internal milling on the crankpins
Internal milling uses an annular cutter with its cutting edges on the inner circumference. US 6,283,687 describes the usual arrangement: the crankshaft does not rotate, while the cutter spins and also travels on a circular path around the crankpin inside it. The cutting speed comes only from the cutter. Because the cutter and journal curve in the same direction, the wrap is large and several edges are often cutting at once, which puts high transverse forces into the workpiece.
Internal milling has advantages too. Because the crankshaft stands still, several pins can be milled at the same time by separate units if they are far enough apart axially. The annular tool is mounted in a support that surrounds it on all sides, which makes the mounting stable, although its inserts are harder to service.
Side-by-side comparison
| Process | Tool | Workpiece motion | C axis needed for pins | Notes from the patents |
|---|---|---|---|---|
| Turning / turn-broaching | Disc with broaching edges, plus a turning edge for turn-broaching | Fast rotation, about 1000 rpm for a passenger-car crankshaft | Not used. Pins would need eccentric chucking | Established for main bearings; clamping force and unbalance are the main difficulties at high speed |
| Internal milling | Annular cutter with inner cutting edges | Usually stationary; variants rotate it as a C axis | Only in the rotating variant | Large wrap, several edges cutting at once, high transverse force; several pins can be cut at once |
| External milling | Disc milling cutter with edges on the outer periphery | Slow rotation, about 10 rpm | Yes | Climb cutting and positive geometry keep forces low; can produce flat outer surfaces |
US 6,283,687 also claims a power figure for external milling. For the size ratios it describes, the positive tool geometry and thin chips lower the cutting forces. The tool drive then needs only about half to one third of the power required for internal milling or rotary turn-broaching. The patent adds that this lowers energy costs and reduces the waste heat from the drives. Treat it as the applicant's comparison for its own configuration, not a general rule.
Crankpin milling parameters: cutting speed and chip thickness
For journals and webs of cast iron or steel milled in the unhardened state with a disc cutter, US 6,283,687 recommends the following ranges.
| Parameter | Minimum | Preferred range |
|---|---|---|
| Cutting speed, roughing | 180 m/min | 250–600 m/min |
| Cutting speed, finishing | 200 m/min | 300–800 m/min |
| Chip thickness | 0.005–0.5 mm overall | 0.1–0.3 mm |
The patent states that these relationships were determined mainly on cast iron of grades GGG60 to GGG80 and may also hold for other materials, such as steel, which use other groups of cutting materials. The ranges are a starting point for process development, not a substitute for trials on your own material and blank.
Why chip thickness comes first
There are two ways to remove metal faster. A higher cutting speed increases the removal rate but, as a rule, shortens tool life. A thicker chip also increases the removal rate, but it raises the cutting forces on the workpiece and so harms dimensional accuracy. US 6,283,687 therefore aims for thin chips.
According to the patent's tests at high-speed milling speeds of 180–800 m/min, the best tool life-cycle performance, meaning the volume of metal removed over the life of a cutting edge, came at chip thicknesses of 0.05–0.4 mm, in particular 0.1–0.2 mm. The tests covered several cutting materials and coatings. Because a milling chip varies in thickness along the cut, the patent applies the target to the average or the maximum chip thickness. Once that thickness is fixed, the cutting speed is kept as high as possible to shorten the cycle.
Two cutters on one crankshaft
Crankpin milling gets more involved when two independent cutters work on the same crankshaft at once. US 6,283,687 shows two disc cutters milling two crankpins at different angular positions. Each cutter can move in X and change its speed independently, but both share one workpiece rotation.
The geometry is not the same at the two contact points. At one pin the crankshaft rotation moves the contact point almost along the cut. At the other a large part of the motion has to be absorbed by the cutter's X movement. With equal cutter speeds and diameters, the second pin would then see a much thinner chip than intended. To keep both chips in the target range, the patent slows the second cutter, in its example to no more than about 30% of the first cutter's speed. When a web face is milled at the same time as a journal, the differences grow, and the controller has to keep adjusting cutter speeds and X motion throughout the cut.
Worked example: cutting speed from a catalog
The cutting speed at the cutter edge follows from the cutter diameter and spindle speed:
v = π·D·n / 1000, with v in m/min, D in mm and n in rpm.
UBright's high-speed crankshaft external milling machine range lists a 700 mm cutter head and a milling spindle speed range of 66–138 rpm for its compact size. The medium size lists a 782 mm cutter head with the same spindle speed range.
| Cutter head D | Spindle speed n | Cutting speed v |
|---|---|---|
| 700 mm | 66 rpm | about 145 m/min |
| 700 mm | 138 rpm | about 303 m/min |
| 782 mm | 66 rpm | about 162 m/min |
| 782 mm | 138 rpm | about 339 m/min |
The upper end of that range sits inside the 250–600 m/min roughing range that US 6,283,687 prefers. The lower end lets a controller slow one cutter to hold the target chip thickness, as described above. The same catalog lists a workpiece spindle speed of 3–30 rpm, in line with the slow rotation that US 6,684,500 describes for external milling.
The disc milling cutter and its inserts
The disc milling cutter is a rotating tool body carrying indexable inserts on its periphery. US 6,283,687 gives an example of such a cutter: a nominal diameter of 800 mm carrying about 120 to 200 inserts, depending on the cutter type and how the inserts are arranged. Different insert types are used for journal surfaces, web faces and undercuts, and each is set at its own position and angle on the tool body.
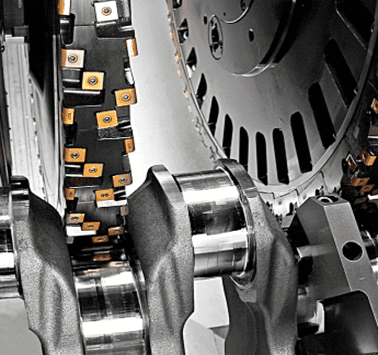
Diameter matters for more than reach. A larger cutter gives a higher cutting speed at the same spindle speed. It also changes how far the cutter wraps around the journal. The patent notes that concave contours can be milled only if their radius of curvature is larger than the cutter radius.
Inserts for unhardened journals
For unhardened cast iron and steel, the inserts in US 6,283,687 are cemented carbide in the ISO K10 to K25 application groups. They carry multilayer coatings built from TiCN, Al₂O₃ and TiN, with total coating thicknesses specified in micrometers for each insert type. The geometry is positive. The patent credits the change from the negative geometry previously used in milling to a positive one, together with thin chips, for lower cutting forces at sufficient tool life.
Servicing a disc cutter is a real cost item. US 6,283,687 notes that reconditioning or resetting cutters with many inserts takes considerable time and is expensive. It therefore counts tool life, alongside machine investment, as part of the machining cost per crankshaft to be minimized.
Cutting hardened crankshafts
For high-speed milling of hardened crankshafts, US 6,283,687 prefers cermet or polycrystalline boron nitride, in particular cubic boron nitride (CBN). It describes carbide inserts with pockets near the cutting edge in which CBN powder is placed and sintered, or CBN segments set along an edge. The patent also states that these cutting materials can run without coolant, which saves on disposal costs.
In this source, PCBN and CBN are introduced for the hardened-part case, although the patent adds that CBN-reinforced inserts can also cut unhardened steel or cast iron. Its detailed insert table for unhardened journals uses coated carbide.
Accuracy and contour control
Accuracy in crankshaft high-speed external milling depends on the part, the fixture, the cutter and the control together. The sources point to three areas.
Clamping, support and cutter balance
US 6,684,500 names the main difficulties of external and rotary milling of crankshafts: clamping or supporting the workpiece rigidly enough, and holding a large, heavy workpiece stably and accurately when it is held on one side only. At high accuracy levels, the true running and balance of the tool and its shaft also become a problem. For turning and turn-broaching the patent lists different difficulties, mainly clamping force and unbalance at high workpiece speed.
US 6,283,687 prefers chucking the crankshaft centrically on its main-journal axis over eccentric chucking on a pin axis, and notes that the crankshaft is usually chucked and driven at both ends. Steady rests, support positions and how the part is driven at each end should be part of any machine review.
Correction points on the pin contour
US 6,283,687 places correction points along the machining path at intervals of about 10–15°, measured from the center of the crankpin being machined. After the first parts of a series are produced, the actual pin contour is measured against the target contour. The machine control then corrects the contour by entering a correction value at each point.
This is a practical way to absorb systematic errors from cutter deflection, support compliance and axis dynamics. It only works if the line has a way to measure the pin contour and feed the result back to the machine. Ask how corrections are entered, stored per part number and audited when parts change.
Flats and recesses on the webs
Because the C axis and the X axis are controlled together, external milling is not limited to round surfaces. US 6,283,687 describes milling planar flats on the web contour by matching the crankshaft's rotational position to the cutter's X position. Such flats can serve to mount counterweights later or to balance the crankshaft in the same clamping. Recessed contours are also possible if their radius of curvature is larger than that of the cutter.
Choosing crankshaft high-speed external milling equipment
Choosing crankshaft high-speed external milling equipment starts with the part and the line. The mechanisms above turn into concrete questions about envelope, axes, cutter and control.
Reading a machine specification
The table below shows how one catalog describes its machine range. UBright lists three sizes of high-speed crankshaft external milling machine for crankshafts, camshafts and similar parts, each with dual milling spindles that move independently on their own X and Z axes. The values are catalog specifications, not results for a particular crankshaft.
| Specification | Compact | Medium | Large |
|---|---|---|---|
| Maximum workpiece length | 800 mm | 1,500 mm | 5,000 mm |
| Maximum main journal diameter | Φ100 mm | Φ125 mm | Φ190 mm |
| Maximum crankpin diameter | Φ75 mm | Φ100 mm | Φ135 mm |
| Cutter head diameter | Φ700 mm | Φ782 mm | Φ1,000 mm |
| Workpiece spindle speed | 3–30 rpm | 3–30 rpm | 21 rpm |
| Milling spindle speed | 66–138 rpm | 66–138 rpm | 105 rpm |
| Milling spindle motor | 37 kW | 41 kW | 41/65 kW |
| X and Z positioning accuracy | 0.01 mm | 0.01 mm | 0.01 mm |
| X and Z repeat positioning accuracy | 0.005 mm | 0.005 mm | 0.005 mm |
| C-axis repeat positioning accuracy | 0.015° | 0.015° | 0.015° |
Three readings matter most. Cutter diameter and spindle speed set the cutting speed, as in the worked example. Workpiece speed confirms that the machine runs the slow-rotation process the patents describe. C-axis repeatability matters because the pin contour is generated by the C and X axes together. Angular accuracy at the C axis turns into position error at the pin, and that error grows with the crank throw.
Pre-purchase checklist
| Check | What to confirm | Why it matters |
|---|---|---|
| Part envelope | Length, main journal and crankpin diameters, crank throw, mass, number of throws | Must fit the X stroke, swing and length of the machine |
| Material and condition | Steel or cast iron; milling before or after hardening | Sets the insert material, cutting speed range and whether any grinding can be reduced |
| Process split | Which surfaces are milled, turned or turn-broached; mains and pins in one clamping or two | Decides the number of machines and handling steps |
| Cutter layout | Number of cutters, diameter, insert count and insert types for journals, webs and undercuts | Drives cutting speed, tool cost and setup time |
| Chip-thickness control | How the control holds chip thickness when two cutters work on different pins | Protects tool life and dimensional accuracy |
| Infeed and run-out | Infeed angle and how far past one revolution the cutter dwells | Avoids force peaks and contour steps at entry and exit |
| Support | Chucks, steady rests and drive at both ends | The crankshaft is the weakest part of the system |
| Contour correction | Measuring method, correction-point spacing and how values are stored per part | Turns first-part measurements into stable pin contours |
| Downstream fit | Stock and condition left for hardening and grinding | Milling quality shows up again at the grinder |
The wider route, from forging through milling, drilling, heat treatment and grinding, is covered in our crankshaft manufacturing solutions.
Frequently asked questions
Is external milling the same as crankshaft following milling?
They describe the same idea. "Following" or "follow-up" milling refers to the cutter following the orbiting crankpin through coordinated C-axis rotation and X-axis motion. "High-speed external milling" refers to the tool type, an external disc cutter, and to the cutting speed it runs at. Both names are used for disc-cutter machines that mill pins while the crankshaft turns slowly.
Does external milling replace crankshaft grinding?
Not in the conventional route. US 6,283,687 describes milling as rough machining, followed by hardening and then grinding to size. The same patent says that high-speed milling of an already hardened crankshaft can give a surface acceptable as the final state, so at least the rough-grinding step can be dropped. It does not claim that finish grinding can be dropped.
Why is chip thickness kept so small?
Thin chips reduce the cutting forces that bend a flexible crankshaft, which protects dimensional accuracy. US 6,283,687 reports the best tool life-cycle performance at chip thicknesses of 0.05–0.4 mm, in particular 0.1–0.2 mm, in tests at 180–800 m/min. Cutting speed is then raised as far as tool life allows.
Which inserts are used for crankpin milling?
For unhardened cast iron and steel, the patent uses coated cemented carbide inserts in the K10 to K25 groups, with multilayer TiCN, Al₂O₃ and TiN coatings and a positive geometry. For hardened crankshafts it prefers cermet or CBN. Insert types differ for journal surfaces, web faces and undercuts.
Summary
- Crankshaft high-speed external milling uses a large disc cutter for the cutting speed while the crankshaft turns slowly as a controlled C axis.
- The cutter follows each crankpin by X-axis motion linked to the crank angle, so pins at different angles are milled in one clamping.
- Patent guidance sets chip thickness first, in the region of 0.1–0.3 mm, then pushes cutting speed toward 250–600 m/min for roughing.
- Climb milling, positive insert geometry and a slow infeed keep forces on the crankshaft low.
- In the conventional crankshaft machining process, milling is followed by hardening and grinding. One patent claims hard milling can remove at least the rough-grinding step, not finish grinding.
- Cutter diameter, spindle speeds and C-axis repeatability are the specification values to read together.
Discuss your crankshaft machining project
If you are planning a crankshaft milling cell or a complete line, send us the part drawing, material and heat-treatment route, annual volume, and which surfaces you want to mill, turn or grind. Our engineers can review the part against our external milling machine range and the rest of the process route. Contact our crankshaft team to start the review.
References
- US6684500B1 – High speed milling and turning/turn broaching/turning and turn broaching — United States patent, priority 1997, granted 2004, via Google Patents. Supports the definitions of rotational broaching, turn-broaching, external milling and rotary milling, the about 10 rpm and about 1000 rpm workpiece speeds, the high-speed milling thresholds, the C-axis requirement and the clamping and balance issues.
- US6283687B1 – Multiple milling on crankshafts — United States patent, priority 1996, granted 2001, via Google Patents. Supports the conventional rough machining, hardening and grinding sequence, the internal milling description, climb milling, the cutting speed and chip thickness ranges, the infeed and correction-point method, insert grades and coatings, the 800 mm cutter example, hard milling and the drive power comparison.
- Development of Multi-grit cBN Grinding Wheel for Crankshaft Grinding — Macerol N., Licentiate thesis, Chalmers University of Technology, 2019. Supports the crankshaft production route of forging, machining, heat treatment and grinding, and the role of grinding as a final operation.